
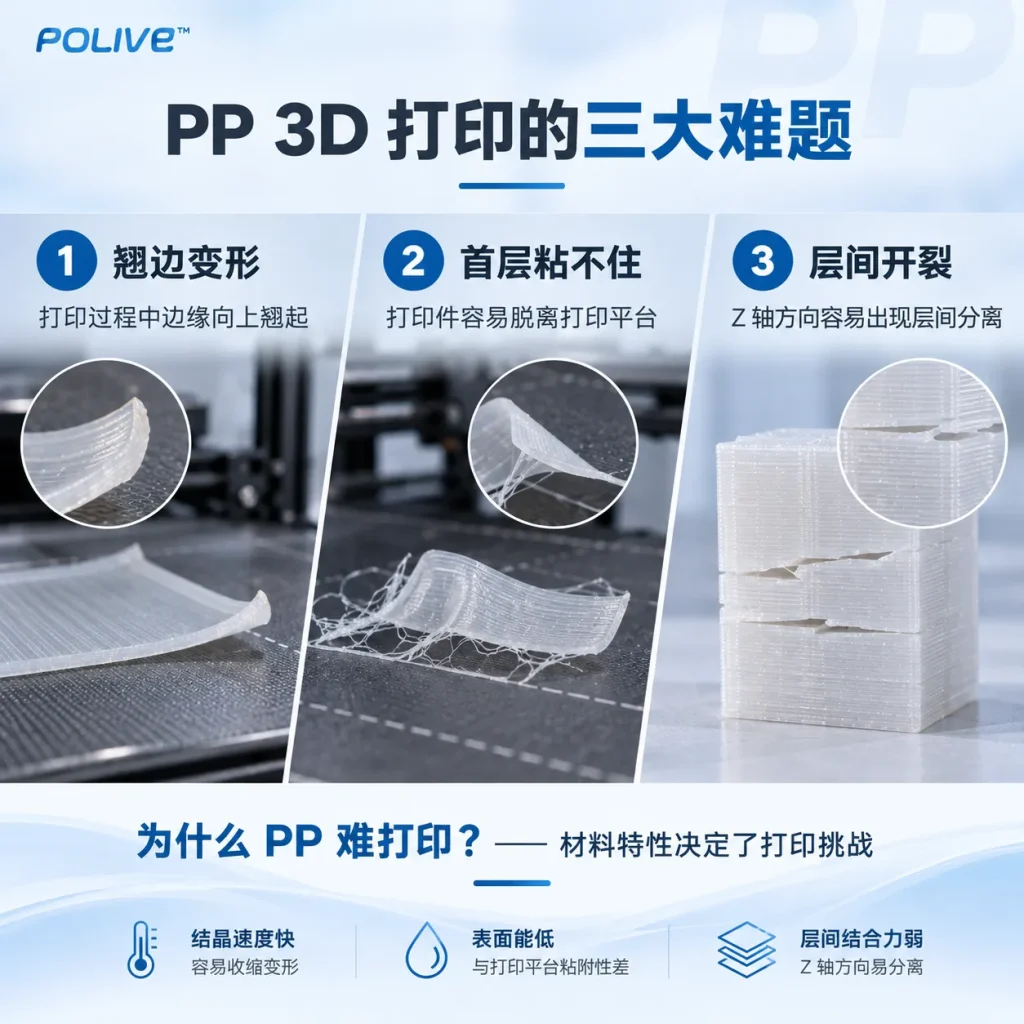
Searching in 3D printing communities “PP filament”, you will often see users discussing several similar questions:
- The first layer is hard to stick to the print bed
- Edges gradually lift during printing
- Large parts are prone to warping
- Interlayer bonding is not ideal after printing
This does not necessarily mean the print parameters are set incorrectly.
PP’s inherent material properties are an important reason why it is difficult to handle in FDM 3D printing.
PP is an engineering plastic with good lightweight, chemical resistance, moisture resistance, and flexibility, but these material advantages do not mean it is naturally suited for FDM printing.
Among them, the three most common challenges are:
shrinkage and warping, first-layer adhesion, and interlayer bonding.
Challenge 1: Shrinkage and warping caused by the semi-crystalline structure
PP is asemi-crystalline polymer.
During cooling, PP undergoes crystallization and volume changes, so the printed part may experience varying degrees of shrinkage in different regions.
For large-size, thin-walled, or structurally complex parts, this shrinkage may further lead to:
- edge lifting / warping at the edges
- bottom deformation
- dimensional deviation
- interlayer stress accumulation
This is also one of the reasons why PP is harder to print than some common FDM materials such as PLA.
It should be noted thatPP’s actual shrinkage rate is not a fixed value that applies to all grades. Material formulation, printing temperature, cooling conditions, part size, and print structure all affect the final result.
Therefore, rather than simply attributing PP’s shrinkage to a certain percentage, it is more important to understand:
PP’s semi-crystalline nature makes it more prone to dimensional changes and internal stress during cooling.
Challenge 2: Low surface energy makes PP hard to adhere to the print bed
Another typical characteristic of PP islow surface energy.
This means the surface adhesion between PP and many common materials is weak.
In FDM printing, this directly affects the first layer:
- the first layer is prone to insufficient adhesion
- edges are prone to lifting during printing
- more noticeable for large parts
- different print beds show large differences in performance with PP
This is also why, when printing PP,the choice of print bed and first-layer parameters are very important.
If the material lacks sufficient first-layer adhesion, the part may gradually detach from the bed during printing even if the subsequent print parameters are set correctly.
Challenge 3: Interlayer bonding requires better material control
FDM 3D printing is not formed in a single step.
The printer forms the final part by depositing molten material layer by layer, so whether the material can form a stable bond between different print layers is very important to the final part’s mechanical properties.
PP’s crystallization behavior, melt flow, and cooling process all affect interlayer bonding.
If interlayer bonding is insufficient, the following may occur:
- insufficient Z-direction strength
- interlayer cracking
- reduced mechanical performance
- the part delaminates after bending or impact
Therefore, PP’s problem is not just about “whether it can be extruded from the nozzle.”
The real challenge is:
how to keep the material stable throughout the entire process of printing, cooling, and interlayer fusion.
How does POLIVE PPPro™ improve these issues?
This is also POLIVE PPPro™ modified PP 3D printing filament‘s core R&D direction.
Compared with ordinary PP, PPPro™ is formulated and performance-tuned to address common material issues in FDM printing, with a focus on:
1. Shrinkage and warping control
By adjusting the material’s crystallization behavior and processing characteristics, the risk of deformation caused by cooling and shrinkage during printing is reduced.
2. Improving first-layer adhesion
Through material design that addresses the adhesion problem caused by PP’s low surface energy, PP achieves more stable first-layer performance under suitable print bed and parameter conditions.
3. Improving interlayer bonding
By optimizing the material’s melting and interlayer fusion performance, a more stable bond is formed between printed layers.
The ultimate goal is not to turn PP into PLA.
Instead, it is:
to make PP more suitable for FDM 3D printing.
No need to change the printer — solve the problem from the material first
The difficulties of traditional PP in FDM printing often mean users need to adjust all of the following at once:
- Printing temperature
- Hotbed temperature
- Print speed
- Cooling
- first-layer parameters
- Build platform
- Printing environment
The significance of modified PP is to start fromthe material itselfto reduce these difficulties.
POLIVE PPPro™’s R&D approach can be summarized as:
not just enabling PP to be printed, but making PP easier to fit into the actual FDM printing workflow.
Of course, the specific print result still depends on the printer, bed, part size, model structure, and print parameters.
Therefore, we recommend performing parameter tests based on the specific equipment, rather than simply copying settings from other materials.
Why choose modified PP?
PP itself has many properties worth using in 3D printing:
low density → lighter
chemical resistance → suitable for more functional environments
moisture resistance → suitable for some outdoor and humid environments
flexibility → suitable for parts that require some elasticity
fatigue resistance → suitable for structures under repeated loads
The real question is:
Ordinary PP is not easy to print stably.
This is also the value of modified PP 3D printing filament.
POLIVE PPPro™: Making PP More Suitable for FDM
POLIVE specializes in PP-modified 3D printing materials.
POLIVE PPPro™ Its goal is to preserve PP’s important material properties while improving the typical problems traditional PP encounters during FDM printing.
From material to printing, what we care about is not just one parameter, but the entire printing process:
material → melting → extrusion → first layer → interlayer fusion → cooling → final part
Only when the entire process is more stable can PP’s material advantages truly translate into the actual performance of 3D-printed parts.
PP being hard to print does not mean it is not worth printing
PP was once considered a relatively difficult material to handle in FDM 3D printing.
Its problems are not mysterious:
semi-crystalline → shrinkage and warping
low surface energy → first-layer adhesion difficulty
crystallization and cooling behavior → interlayer bonding control difficulty
But these are precisely the areas where material modification can play a role.
POLIVE PPPro™’s core goal is to turn PP from a “hard-to-print engineering plastic” into a 3D printing material that is far more suitable for real-world FDM use.
If you are looking for a PP filament more suitable for FDM printing, you can learn more about POLIVE PPPro™.
PP 以前为什么这么难打?
集中在三件事:半结晶带来的收缩和翘边、低表面能导致首层粘不住、层间结合偏弱。这三点互相叠加,所以过去常要靠加热床和封箱去硬压。
不加热、不封箱,翘边靠什么压住?
从模型和平台两头下手:直角改圆角、底部加厚做老鼠耳朵、增大底部接触面积、壁厚尽量均匀;平台加裙边,配合 PPLOCK26811 专用胶水。PP 冷却要散掉大量热,空调房里开门开盖、开放机架反而更利于散热定型。
首层粘不住,一定要加热床吗?
不用。把 PPLOCK26811 薄涂在平台上,等几分钟干透后直接打印即可;一次涂抹可以连续打多次,需要清洁时用酒精擦掉就行。这比靠温度去烫住首层更稳定,也不挑机器。
层间结合差,是不是只能靠封箱保温?
封箱会拖慢 PP 散热,跟我们想要的冷却节奏相反。更有效的还是打印路径和零件设计:壁厚均匀、避免截面急剧变化、拐角过渡平缓,收缩应力小了,层间自然更稳。
Related Reading
- 什么是改性 PP?POLIVE PPPro™ 到底改了什么?
- PP 3D 打印参数怎么设置?PPPro™ 参数指南
- PP or PLA: Which Should You Actually Choose?
- PP 密度为什么只有约 0.90 g/cm³?



